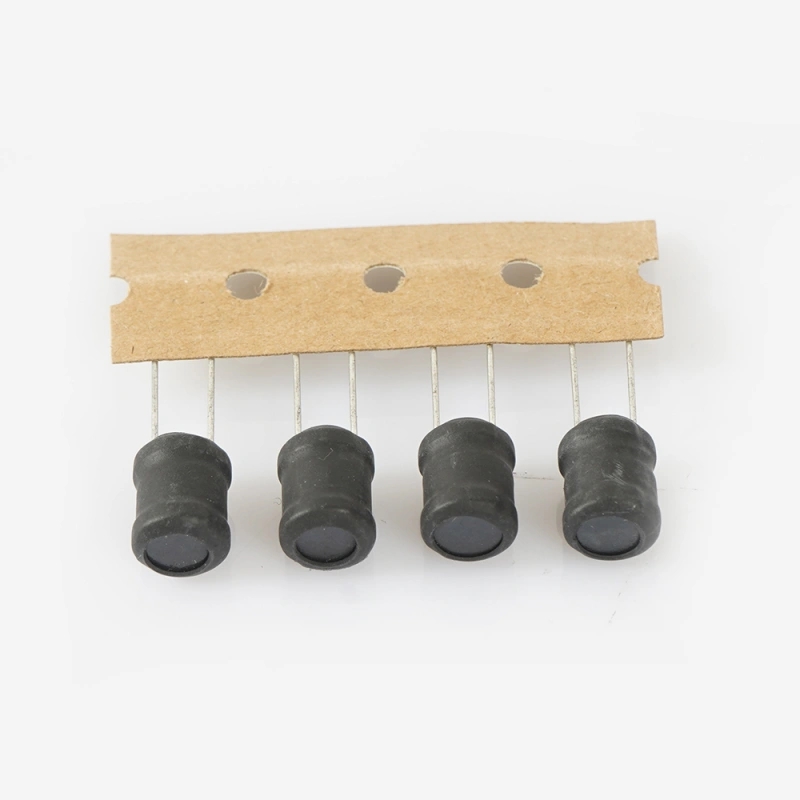
Drum Inductor Overview
A Drum Inductor is a practical choice when a circuit needs compact inductive parts for filtering, energy handling, or noise control on a printed circuit board. In through-hole assemblies, buyers often face a familiar problem: they need passive components that are easy to insert, stable in assembly, and suitable for repeated production without adding complexity to the line. Drum-style inductors address that need by offering a simple leaded form factor that can be used in power supplies, signal conditioning stages, and general electronic equipment.
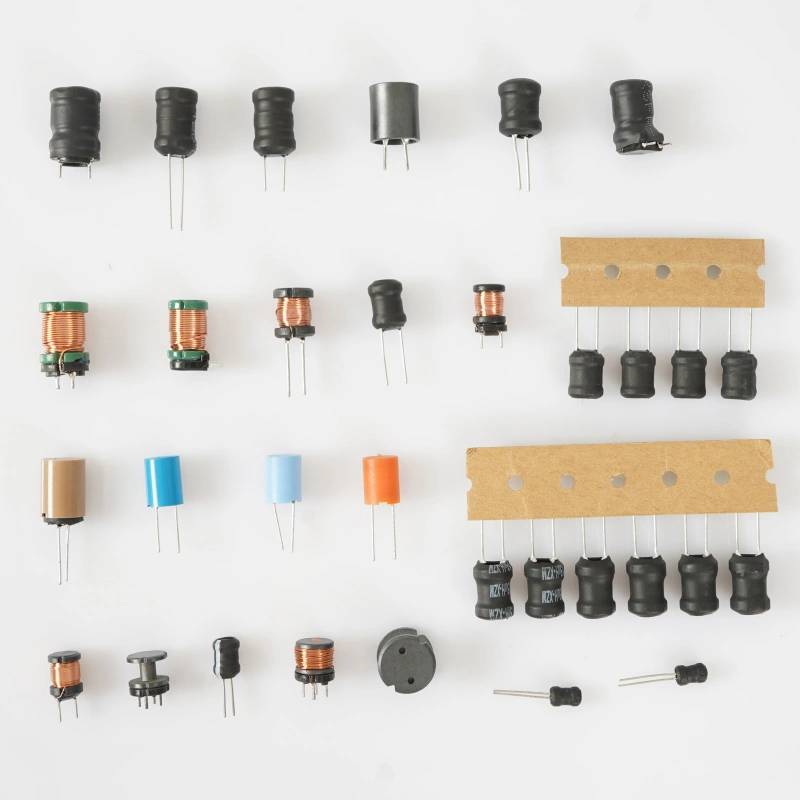
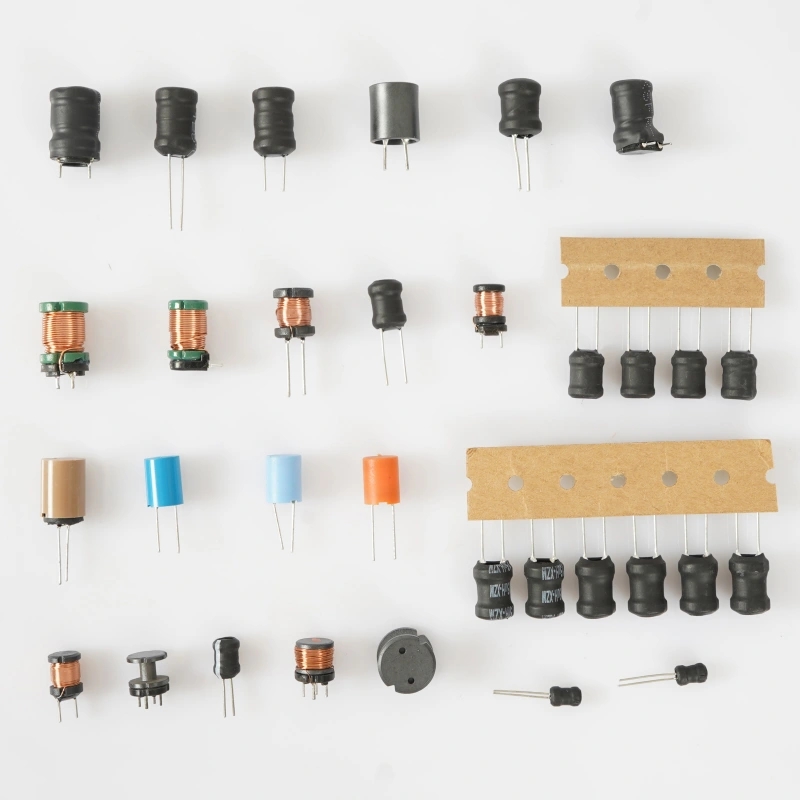
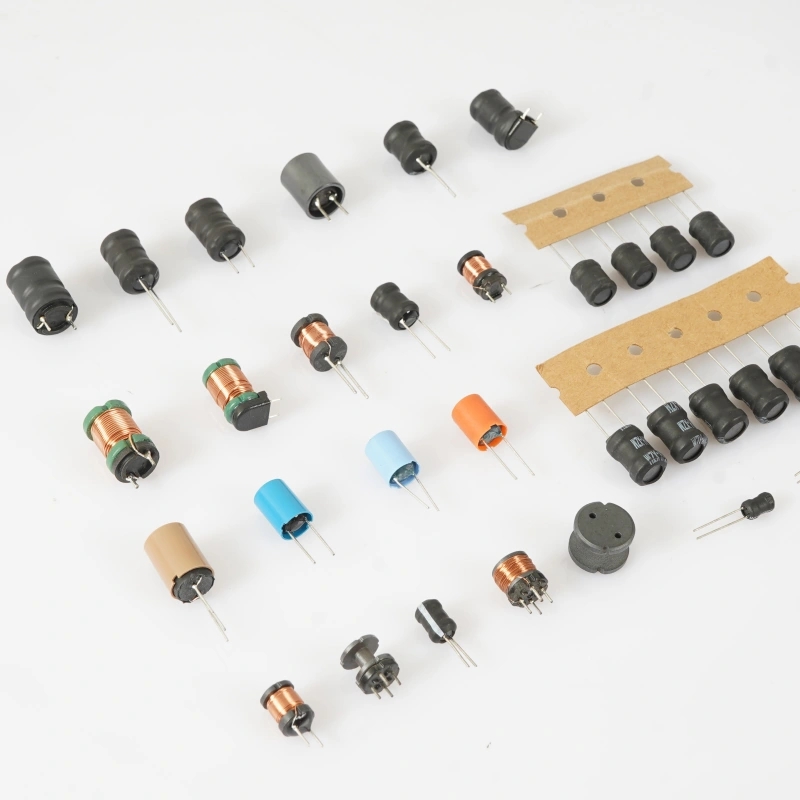
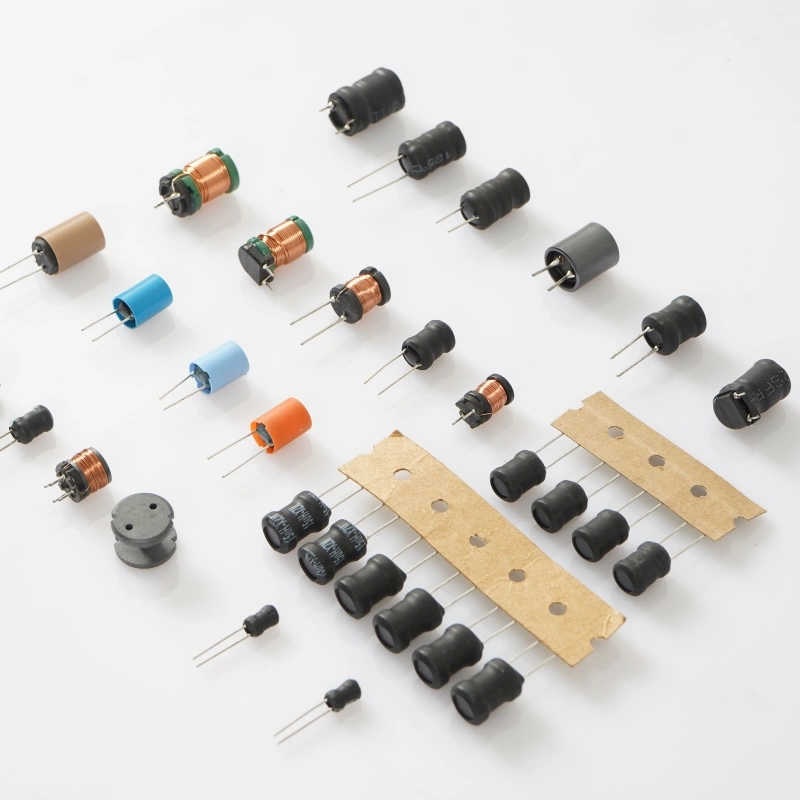
The visible product data here also points to related through-hole passive components presented in different package formats, including strip-packed cylindrical parts and small coil-like bodies. Because the image set shows multiple component styles together, the safest reading is that this page reflects the broader category of through-hole passive electronic components used in PCB assembly, with drum-style inductors as the main reference point.
Product Reference and Visible Construction
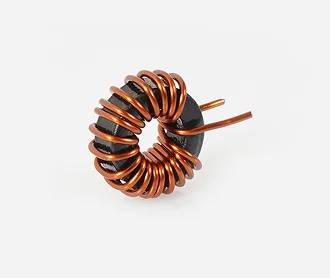
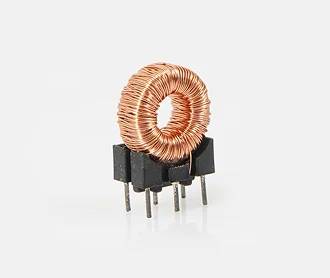
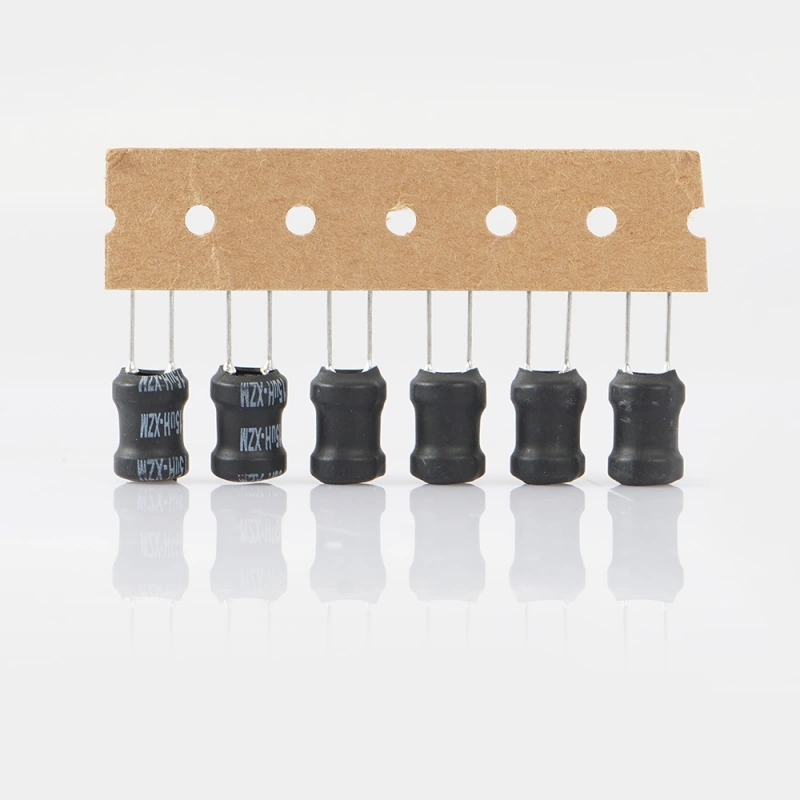
Drum inductors typically use a wound conductor around a bobbin or core structure, then seal or mold the body for handling and assembly. In the supplied product information, the visible parts include cylindrical black bodies, copper-wound coil forms, and leaded components packaged on carrier strips. Some pieces appear loose, while others are aligned for automated insertion.
From the image-based notes, the most reliable observations are structural rather than electrical: the parts have two wire leads, the bodies are cylindrical or can-shaped, and the packaging includes strip-mounted formats that help feeding equipment handle the components during PCB assembly. Exact inductance values, tolerances, saturation current, or core materials are not identifiable from the image alone and should not be assumed.
What the format tells a buyer
For procurement and production teams, the key value of this form factor is compatibility. Through-hole parts can be inserted manually, semi-automatically, or with production equipment before soldering. Strip packaging reduces handling errors, keeps leads aligned, and makes high-volume placement more consistent. That is especially useful in assemblies where board robustness, reworkability, or legacy process compatibility still matters.
Key Specifications and Capabilities
Because the exact part numbers are not visible, the specification discussion should focus on capabilities commonly expected from drum inductors and similar through-hole passive components:
- Two-lead through-hole construction for PCB mounting
- Cylindrical or molded body geometry for compact placement
- Compatibility with hand insertion, wave soldering, or other through-hole workflows
- Potential use in filtering, energy storage, and EMI suppression circuits
- Availability in bulk, loose, or tape/strip packaging depending on production method
In the provided material, several pieces are shown in tape-style carrier strips with punched holes. That format is a practical detail for assembly planning because it supports mechanical feeding and organized inventory management. A buyer comparing options should confirm lead spacing, body size, packaging format, and the exact passive function before release to production.
Materials and Finish Options
Visible construction details suggest a mix of black molded housings, matte metal lead finishes, copper-colored wound elements, and some epoxy-coated cylindrical bodies. Those surface characteristics are common across many leaded passive components, but the internal materials cannot be verified from the image alone.
In general, drum inductors and related passive components may use combinations of ferrite, molded resin, enamelled copper wire, tinned copper leads, or encapsulating compounds. Finish options are usually driven by assembly needs rather than appearance alone. A tinned lead finish helps solderability. A molded or coated body helps mechanical stability. A carrier-strip package protects lead alignment during storage and feeding.
Packaging formats visible in the supplied data
The supplied information shows three useful handling styles: loose components for manual work, strip-packed parts for automated insertion, and mixed passive component groupings for comparison. That matters because packaging is not just logistics; it affects line speed, pick reliability, and operator effort.
Manufacturing Process and Assembly Relevance
For a drum inductor, the basic manufacturing route normally includes winding conductor wire, forming or preparing the core or bobbin, securing the winding, adding leads, and finishing the body for assembly. After that, components may be packed loose or mounted on carrier strips for downstream insertion. The exact process depends on the electrical target and the production volume.
The visible product set suggests a manufacturing and packaging environment focused on PCB assembly support rather than finished end-user retail packaging. That is consistent with passive component supply for industrial electronics, repair stock, OEM builds, and contract manufacturing. In this context, packaging uniformity and lead integrity are important because they influence insertion quality and solder joint consistency.
Application Scenarios
Drum inductors and neighboring through-hole passive parts are commonly used in circuits where a board needs dependable passive behavior with straightforward assembly. Typical use scenarios include:
- Power supply filtering and smoothing stages
- Signal conditioning and noise suppression
- EMI reduction in control boards and interface circuits
- General electronics builds that still rely on through-hole assembly
- Repair, replacement, and service inventories for legacy equipment
Because the supplied image data includes other passive components such as likely capacitors and ferrite/bead-style parts, it is reasonable to treat the full set as representative of a PCB-level passive component family. Buyers sourcing this category often need to match the part to the circuit role first, then confirm physical packaging to fit the assembly process.
Quality Control Considerations
For passive components, quality control is about repeatability and fit, not only appearance. A buyer should verify lead straightness, body consistency, package integrity, and feed compatibility. If the parts will be machine inserted, carrier strip accuracy becomes important. If the parts will be hand assembled, body size and lead length matter more.
From the supplied information, we can confirm visible consistency in lead count, cylindrical body style, and strip-mounted arrangement for some items. We cannot confirm electrical test data, exact tolerance bands, temperature class, or compliance markings. Those should be requested from the supplier’s datasheet or inspection record before a production decision is made.
What to ask before ordering
- Exact component type and electrical function
- Inductance or other relevant electrical value
- Lead spacing and overall dimensions
- Packaging format and reel or strip quantity
- Compatibility with wave soldering or insertion equipment
Customization and Sourcing Guidance
When specifying a drum inductor for a manufacturing program, the main customization factors are usually electrical value, physical size, lead form, and packaging method. A larger core or winding can change performance, but it can also affect board footprint and insertion clearance. A different lead length or pitch may be needed for an existing PCB pattern. Packaging can also be tailored for manual line work or automated feed systems.
For mixed passive assemblies, buyers should separate the sourcing requirements by part family. The provided image data includes parts that are likely not all inductors, so it is better to confirm each BOM line individually. This avoids the common mistake of using visual similarity as a substitute for specification control.
Buyer Decision Factors
When evaluating a Drum Inductor or related through-hole passive component, the most important decision factors are practical:
- Does the component match the circuit function?
- Will the body size fit the available PCB area?
- Is the lead format compatible with the assembly process?
- Can the supplier provide stable packaging for production use?
- Are the electrical ratings documented in a datasheet?
For high-volume manufacturing, consistency in packaging and lead geometry may matter as much as the nominal electrical value. For maintenance or prototype work, availability and handling convenience may be more important. Matching the sourcing decision to the actual production stage usually prevents delays later in assembly.
Conclusion and Next Step
The supplied product information points to a family of through-hole passive components, with drum inductor-style parts represented by cylindrical bodies, two-lead construction, and tape or strip packaging for PCB assembly. While the image does not expose exact electrical ratings, it does show the practical details that matter to procurement and manufacturing teams: package style, lead configuration, and feed-ready presentation.
If you are selecting a Drum Inductor for a board design or replenishing passive inventory, the next step is to confirm the datasheet, lead spacing, and packaging format against your assembly method. For supplier inquiries, request the exact part number, electrical specification, and feed format so the component can be matched correctly to the production line.
Contact your sourcing team or component supplier with the target PCB requirements, and use the confirmed specification set to lock down the right passive part before mass assembly starts.